
2024-06-13 hits:0 source:corten steel fabricators
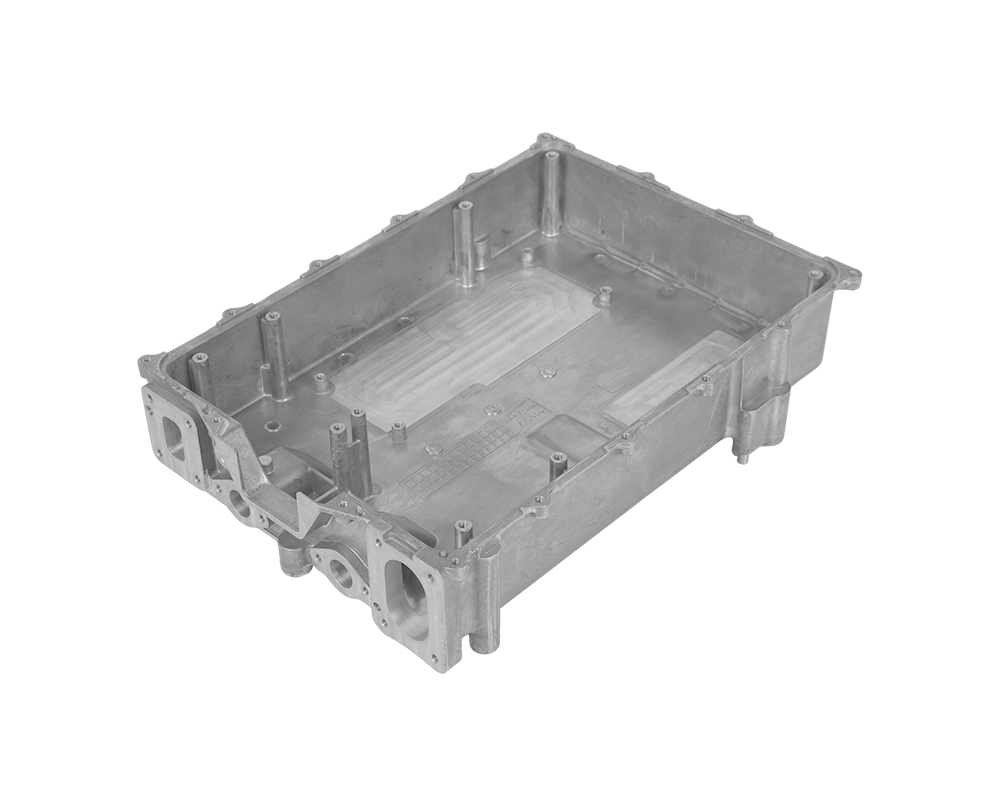
The location of casting peeling is often on larger flat surfaces, curved surfaces, or near sharp corners. Obvious peeling can only be clearly observed after shot blasting. So what is the reason for peeling? Firstly, due to uneven filling or slow flow caused by splashing, the metal liquid entering the mold cavity first fails to fully fuse with the subsequent metal liquid, resulting in weak bonding of the substrate and causing surface peeling. 2、 High impact pressure or mold deformation during die casting. 3、 The mold temperature is not suitable, or the runner design is unreasonable. 4、 The impact of release agents, different release agents have different focuses, and some release agents may have an impact on peeling. 5、 Peeling is also related to shot blasting, which can be improved by changing the material of shot blasting or reducing the time of shot blasting.

Read recommendations:
aluminium fabrication company profile
aluminium door frame extrusions
polypropylene injection molding
Fabrication of New Energy Battery Housings using Industrial Pure Aluminum Die-Casting
 +86 18879690228
Email: Harvey@greenwayalu.com
Headquarters: Floor 5, Building B,GS Industry Park, Longhua District, Shenzhen518109,China.
Dongguan factory: Shishuikou Industrial Park, Qiaotou Town, Dongguan City, Guangdong Province,China.
©2013 GREENWAY All rights reserved




 CN
 Home >
